Print Stats
Print Stats reads a G-code file, or a toolpath, and reports the printed length, the travel length, the amount of material in cubic centimetres and grams, an estimated print time, and a table with one row per layer. The report is a quick check before a long print.
Panel: 5 Analyze. Nickname: Stats. Compute button: no (runs on every change).
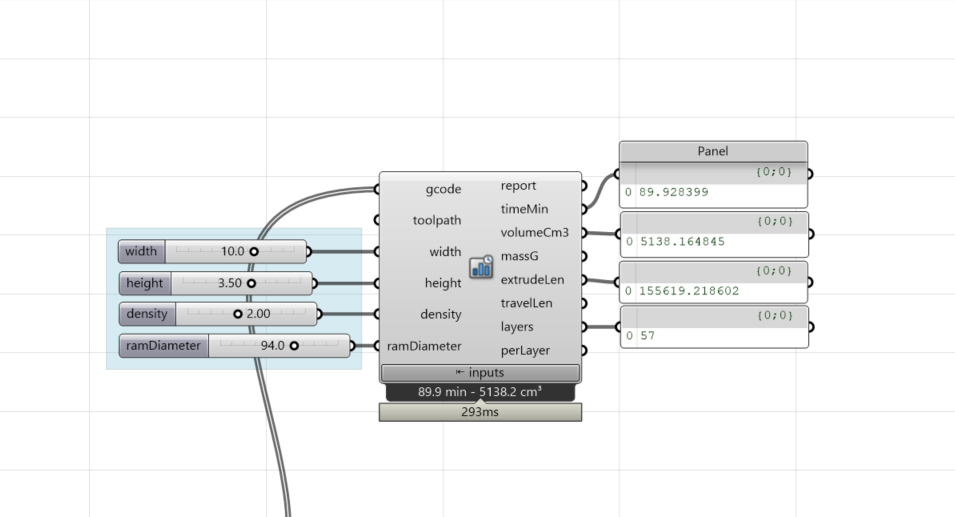
Inputs
| Name | Type | Default | Description |
|---|---|---|---|
gcode |
Text (list) | G-code as one string or a list of lines. Feeds per move are honored | |
toolpath |
Curve (tree) | Toolpath curve tree in Rhino document units, used only when gcode is empty | |
width |
Number | 10 | Layer width in mm for geometric volume estimates |
height |
Number | 0 | Layer height, mm (0 = auto from the Z steps) |
density |
Number | 2 | Material density, g/cm³ (clay ≈ 2.0) |
ramDiameter |
Number | 94 | Ram cartridge bore in mm for volume from G-code E travel (0 = estimate from layer width and height) |
Optional group: Feed override inputs
Right-click the component to switch this group on. The inputs appear only while the group is enabled.
| Name | Type | Default | Description |
|---|---|---|---|
printFeed |
Number | 25 | Default print feed where the source has none, mm/s |
travelFeed |
Number | 60 | Default travel speed in mm/s where the source has no feedrate |
accel |
Number | 0 | XY acceleration in mm/s^2 for estimating acceleration and corner delays (0 = commanded speeds only) |
Optional group: Robot Definition input
Right-click the component to switch this group on. The inputs appear only while the group is enabled.
| Name | Type | Description |
|---|---|---|
robot |
Text | Optional Robot Definition. With a kinematic profile the estimate also honors the robot’s joint speed limits, not the Cartesian feed alone |
Outputs
| Name | Type | Description |
|---|---|---|
report |
Text | Readable statistics report. Connect a panel |
timeMin |
Number | Estimated duration in min, using joint speed limits when available, otherwise acceleration or commanded speeds |
volumeCm3 |
Number | Extruded volume, cm³ |
massG |
Number | Extruded mass, g |
extrudeLen |
Number | Total nozzle path length while extruding, mm |
travelLen |
Number | Travel length, mm |
layers |
Integer | Layer count |
perLayer |
Number (tree) | One branch per layer: Z in mm, extrusion length in mm, time in min |
Back to Components.